How to Choose the Best Extruded Aluminum Profiles?

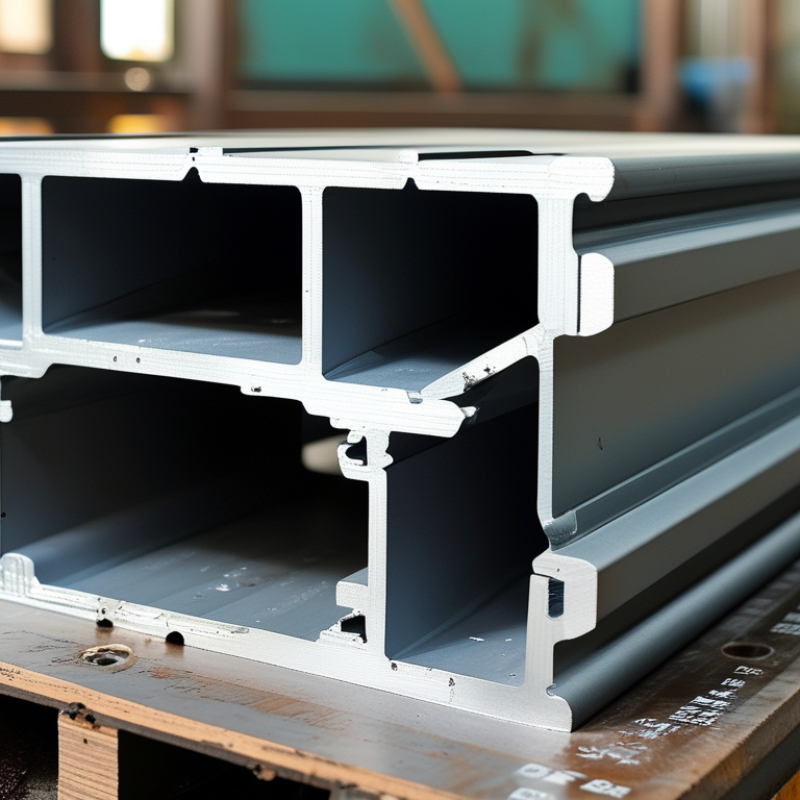
Choosing the right Extruded Aluminum Profiles involves more than comparing prices or browsing attractive product photos. A suitable profile must match the project’s load, dimensions, environment, and manufacturing requirements. Alloy selection matters. For example, 6063 aluminum often provides a smooth surface for architectural frames, while 6061 offers greater strength for demanding structural applications. Temper, wall thickness, and cross-sectional shape also influence performance.

Start with the real working conditions. Will the profile support a machine guard, carry a panel, or form a lightweight enclosure? Measure expected loads, connection points, vibration, and exposure to moisture or chemicals. Small details matter. A thin wall may reduce weight but create unwanted deflection. A complex shape may improve stiffness, yet increase tooling and machining costs.

Surface finish deserves careful attention. Anodizing can improve appearance and resistance to everyday wear, while powder coating offers broader color choices. However, neither finish can correct poor extrusion quality. Check dimensional tolerances, straightness, surface defects, and cut accuracy before approving large quantities. Reliable suppliers should provide material certificates, inspection records, and clear information about alloy, temper, and production standards.

Do not trust appearance alone.

In practice, selection is rarely perfect on the first attempt. A profile can meet a drawing yet perform poorly after assembly. Engineers should test a sample under realistic conditions, including fasteners, brackets, and actual span lengths. It is also wise to review supplier experience, communication, tooling capability, and delivery consistency. The best choice balances strength, finish, cost, availability, and long-term reliability—not merely the lowest quotation.
How to Choose the Best Extruded Aluminum Profiles?

Define the Load Case and Size the Profile for a 3:1 Safety Factor

Choosing an extruded aluminum profile starts with the load case, not the catalog shape. Record the load, span, support condition, direction, and application point. Include equipment weight, moving loads, impact, vibration, and eccentric loading. A 300 N load placed 400 mm from a support creates 120 N·m of bending moment. That detail can change the required profile dramatically.

Use a 3:1 safety factor against yield strength. The Aluminum Association’s Aluminum Standards and Data, 2023 edition, lists 6061-T6 extrusions with a minimum yield strength near 241 MPa. Dividing by three gives an approximate allowable bending stress of 80 MPa. This is only a screening value. Confirm the exact alloy, temper, wall thickness, and surface condition before approval. Local buckling and joint failure may occur first.

Deflection also deserves attention. A profile can satisfy the stress check and still feel weak, misalign equipment, or produce visible sag. Check second moment of area, not only the outer dimensions. For long spans, limit deflection according to the equipment function, often around span/360 for precise structures. Connections need separate review because bolts, slots, and corner joints reduce real stiffness. I have seen designs pass a simple static calculation but fail after vibration testing. That is why the 3:1 factor should support engineering judgment, not replace it. Reflect on the worst credible load, including the one your first calculation overlooked.

Choose Alloy and Temper: 6063-T5 ≈186 MPa vs 6061-T6 ≈290 MPa

How to Choose the Best Extruded Aluminum Profiles?

Choose Alloy and Temper: 6063-T5 ≈186 MPa vs 6061-T6 ≈290 MPa

The alloy and temper determine how an aluminum profile performs under load. 6063-T5 typically offers about 186 MPa tensile strength, depending on the specification and section size. It extrudes smoothly and produces clean, attractive surfaces. This makes it suitable for frames, covers, light partitions, and architectural sections. 6061-T6 reaches approximately 290 MPa tensile strength. It is stronger and better suited to brackets, machine structures, and load-bearing components. However, its extrusion process can be less forgiving. Do not choose strength alone.

Tips: Check the required load, span, wall thickness, and joining method before selecting an alloy. Ask for a material certificate and confirm the temper condition. Values can vary between standards and suppliers. Compare the actual profile drawing, not only the alloy label.

In practical design work, I once selected 6063-T5 for a long frame because its surface looked ideal. The frame later showed excessive deflection. The calculation was correct, but the wall thickness was too small. That mistake changed my process. I now review bending, buckling, fastener loads, and machining requirements together. 6061-T6 may solve the strength problem, but it can increase cutting difficulty and cost. Corrosion exposure also matters, especially near moisture or chemicals. A profile that appears overdesigned may still need better connections. Pay attention to the details.

Optimize Section Geometry Using the Second Moment of Area, I = bh³/12

How to Choose the Best Extruded Aluminum Profiles?

For a rectangular section, the second moment of area is I = bh³/12. Here, b is width and h is height from the bending axis. Height matters dramatically because it is raised to the third power. Doubling h increases I eight times, while doubling b only doubles it. Orientation matters. A 40 mm × 20 mm profile resists bending far better when its 40 mm side stands vertically.

In practical profile selection

I first identify the bending direction, span, load, and allowable deflection. Then I compare profiles using I, section modulus, mass, and connection space. A taller rib may reduce deflection, but it can create local buckling or complicate machining. Hollow chambers often improve stiffness efficiently, although sharp corners and thin walls may weaken real performance. The formula is useful, but it is not enough.

Industry data also supports careful material efficiency.

The International Aluminium Institute’s 2023 pathway report states that recycled aluminum requires about 5% of the energy used for primary aluminum production. The U.S. Geological Survey’s Mineral Commodity Summaries 2024 reported approximately 70 million metric tons of global primary aluminum production in 2023. These figures make unnecessary mass worth questioning. I still verify the selected extrusion through finite-element analysis, tolerance review, and prototype loading. Small assumptions can distort results. A perfect calculation can still meet an imperfect profile.

Specify Tolerances Under EN 755-9 and Maintain Walls Above 1.5 mm

Choosing an extruded aluminum profile starts with tolerances, not appearance. EN 755-9 defines dimensional limits for extruded profiles, including wall thickness, straightness, twist, and angular accuracy. The permitted deviation depends on the nominal size and profile geometry. Do not copy one tolerance across every section.

Keep wall thickness above 1.5 mm whenever possible. Thin walls can cool unevenly during extrusion, increasing distortion and dimensional variation. They may also dent during cutting, transport, or assembly. A 1.6 mm wall can behave very differently from a 1.2 mm wall, even when both appear adequate on a drawing. Ask the extruder to confirm achievable tolerances before finalizing the design. Real production feedback matters more than optimistic CAD assumptions.

Material efficiency still matters. The International Aluminium Institute reports that recycled aluminum requires about 5% of the energy used for primary aluminum production. However, reducing thickness too aggressively can create more scrap, rework, and replacement parts. That weakens the environmental calculation. Specify inspection points clearly, especially on visible faces and joining areas. Include sampling frequency, measurement tools, and acceptance limits. A laser scan may reveal bowing that a single caliper misses. One practical weakness remains: EN 755-9 compliance does not guarantee perfect assembly. Review the complete tolerance stack with the fabricator.

How to Choose the Best Extruded Aluminum Profiles?

Specify Tolerances Under EN 755-9 and Maintain Walls Above 1.5 mm

A wall thickness above 1.5 mm generally provides a more practical starting point for profile design, helping reduce extrusion and dimensional risks. The 1.5 mm line is a design threshold, not a universal EN 755-9 tolerance requirement. Specify the applicable EN 755-9 tolerance class and dimensional limits according to the selected profile geometry, alloy, and extrusion process.

Select Finishing: 10–25 μm Anodizing or 60–120 μm Powder Coating

Choosing extruded aluminum profiles starts with the finishing specification, not color alone. A 10–25 μm anodized layer bonds with the aluminum surface and preserves a crisp metallic appearance. It suits interior frames, light outdoor exposure, and projects needing stable dimensions. The coating is thin, so scratches can reveal the substrate. That detail is easy to underestimate. Anodizing also follows the profile’s texture, including die lines and small surface marks. Ask for sample lengths before approving production. Samples matter.

Powder coating at 60–120 μm creates a noticeably thicker protective film. It offers broad color choices, stronger visual coverage, and useful resistance against handling damage. This option often fits façades, equipment enclosures, railings, and humid environments. However, thickness can affect tight assemblies, drainage gaps, and sliding interfaces. Measure critical dimensions after coating, not only before it. Pretreatment matters. Poor cleaning can cause blistering or weak adhesion, even with a thick finish. Specify gloss level, texture, edge coverage, and inspection method in writing.

From project inspections, I have found that finish selection fails when exposure conditions remain vague. “Outdoor use” is not enough. Consider sunlight, salt air, abrasion, cleaning chemicals, and expected service life. Request adhesion checks, coating-thickness readings, and visual inspection under consistent lighting. One imperfect but useful practice is testing a small batch first. It can reveal color variation between profile faces and concealed areas. I would also review whether 120 μm is genuinely necessary; extra thickness may add cost without improving performance. Choose the finish around the environment, fit, and maintenance plan.

How to Choose the Best Extruded Aluminum Profiles? - Select Finishing: 10–25 μm Anodizing or 60–120 μm Powder Coating

The right finish depends on the required appearance, exposure conditions, dimensional tolerance, wear resistance, and production requirements. The values below are typical specification ranges and should be confirmed for the selected alloy, surface preparation, color, and application environment.

Selection Dimension Anodizing
10–25 μm
Powder Coating
60–120 μm
Practical Selection Guidance
Coating Type Electrochemically formed aluminum oxide layer integrated with the aluminum surface. Thermoset polymer film applied electrostatically and cured by heat. Choose anodizing for a metallic, substrate-integrated finish; choose powder coating for a thicker decorative and protective film.
Typical Film Thickness 10–25 μm
Common architectural ranges are approximately 10–20 μm, with higher thicknesses used for more demanding conditions.
60–120 μm
Final thickness varies with profile geometry, color, powder formulation, and application requirements.
Powder coating adds substantially more surface build-up, which should be considered for tight fits and mating parts.
Surface Appearance Metallic appearance with visible aluminum grain; available in clear, bronze, black, and other anodized tones. Wide range of solid colors, textures, gloss levels, and special effects; can provide a more uniform opaque appearance. Use anodizing when retaining the natural metallic character is important. Use powder coating when color flexibility is the priority.
Color Consistency Color can vary with alloy composition, extrusion batch, surface texture, and anodizing lot. Generally offers broad color matching capability, but batch-to-batch variation can still occur. For large visible projects, approve a physical sample and control all profiles within the same color and production batch where possible.
UV and Weathering Very good resistance to sunlight because the finish is inorganic and does not peel as a polymer film. Good to very good resistance when an exterior-grade powder formulation is selected; performance depends on resin, pigment, film thickness, and exposure. For strong sunlight or long exterior service, specify a tested exterior-grade system and define color-retention and gloss requirements.
Corrosion Protection Provides a stable oxide barrier, but damaged areas and unsuitable alloy conditions may reduce protection. Provides a continuous barrier when pretreatment and curing are properly controlled; scratches or exposed edges may allow localized corrosion. For coastal or high-humidity locations, require suitable pretreatment, drainage design, edge coverage, and verification testing.
Scratch and Wear Resistance Hard surface with good resistance to abrasion and handling wear; the finish cannot be repaired by simply recoating the damaged area. Good impact and abrasion performance when correctly formulated and cured; deep scratches can expose the aluminum beneath. Select anodizing for frequent light contact and a hard metallic surface. Select powder coating when impact resistance and color options are more important.
Dimensional Effect Typically causes limited dimensional change because the oxide layer grows partly into the aluminum and partly outward. Adds the full dry-film thickness to the coated surface and may affect sliding fits, joints, and insertion clearances. Define masking areas and allowable build-up on precision interfaces before production.
Repairability Local repairs are difficult to make invisible; replacement or controlled refinishing is usually preferred. Small defects may be touched up, although repaired areas may differ in color, gloss, and texture from the original coating. For visible architectural parts, order spare profiles or establish an approved repair procedure before installation.
Edge and Corner Coverage Follows the aluminum surface closely, but sharp edges may show color or thickness differences. Can provide good coverage, although sharp edges, recesses, and Faraday-cage areas require careful powder application. Use suitable edge radii and avoid unnecessarily sharp corners in the extrusion design.
Typical Applications Window and door frames, curtain wall components, railings, trims, furniture details, and products requiring a metallic finish. Building facades, outdoor frames, fencing, equipment housings, transport components, and products requiring broad color selection. Match the finish to the environment, visual requirements, maintenance plan, and expected handling conditions.
Quality Checks Film thickness, color and appearance, sealing quality, abrasion resistance, and corrosion resistance may be checked according to the agreed specification. Film thickness, gloss, color, adhesion, curing, impact resistance, and corrosion resistance may be checked according to the agreed specification. Specify acceptance criteria before ordering. Common references include ISO 7599 for anodizing and ISO 2360, ISO 2409, or ASTM D3359 for relevant coating measurements and adhesion checks.
Best Overall Choice When... You need a durable metallic appearance, low surface build-up, and strong resistance to normal outdoor weathering. You need a thick protective film, extensive color and texture choices, and a finish suitable for many exterior or industrial applications. Neither finish is universally better; the best choice is determined by exposure, appearance, dimensional tolerances, and lifecycle requirements.

Specification note: Coating performance is affected by aluminum alloy, extrusion surface quality, cleaning and pretreatment, sealing or curing conditions, profile geometry, installation, and local climate. Always approve representative samples and define measurable acceptance criteria before mass production.

Select Electrical Logo
Since 1988

Select Electrical Ltd. © Copyright 1988-2025