How to Weld 304 Stainless Steel Successfully?
Welding 304 Stainless Steel successfully requires more than choosing the correct electrode or filler wire. The process depends on cleanliness, controlled heat, stable shielding gas, and careful joint preparation. A fingerprint, grinding dust, or carbon-steel particle can leave contamination behind. That small mistake may later appear as staining, porosity, or corrosion.
John C. Lippold, a recognized authority in stainless steel welding, offers a practical warning: “The welding process must be controlled to preserve stainless steel’s corrosion resistance.” His point reaches beyond technique. Excessive heat can produce distortion, heavy discoloration, and an unfavorable heat-affected zone. Poor gas coverage can damage the weld surface before the operator notices. Welding 304 Stainless Steel therefore demands observation during every stage, not only inspection after cooling.
This guide examines preparation, fit-up, shielding, filler selection, amperage, travel speed, and post-weld cleaning. It also considers common process differences between TIG, MIG, and stick welding. Some recommendations may require adjustment. Material thickness, joint design, equipment condition, and workshop airflow can change the result. That uncertainty matters.
A clean, bright bead is not automatically a reliable weld. Appearance can mislead. Test pieces, measured settings, and documented results provide stronger evidence. Even experienced welders sometimes rush the setup. That is worth admitting. Better results usually come from slowing down, checking the details, and correcting weak habits before they become permanent.
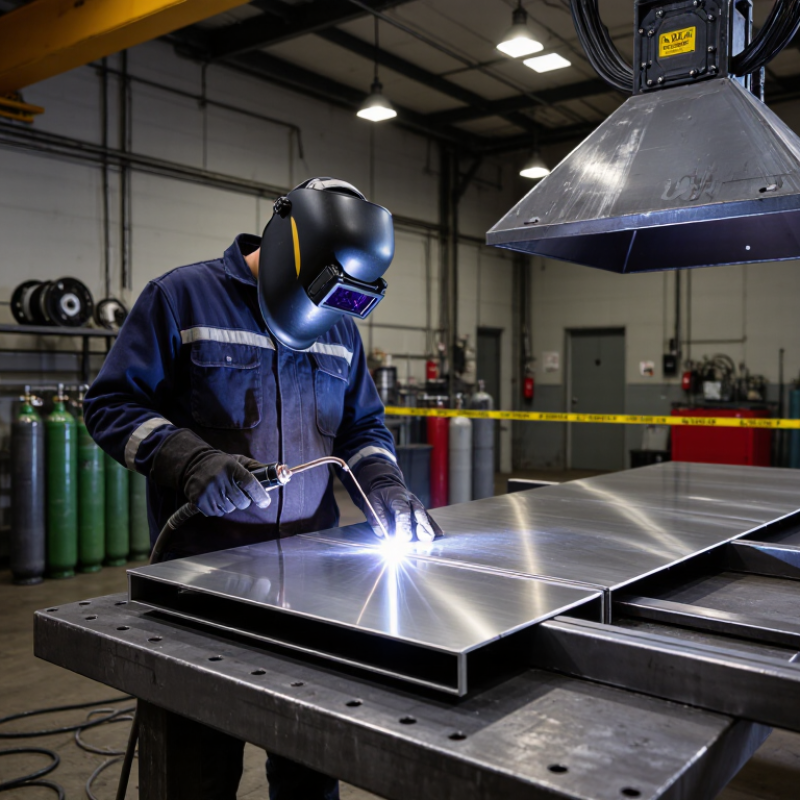
Table of Contents [Hide]
Understanding 304 Stainless Steel and Its Welding Characteristics
304 stainless steel is an austenitic alloy containing chromium and nickel. Its chromium content forms a thin, self-healing oxide layer that protects the surface from corrosion. Nickel helps maintain its ductility and stable austenitic structure during fabrication.
This steel welds readily with TIG, MIG, or covered-electrode processes. However, it expands more than mild steel when heated, so distortion can appear beside a short weld. I use clean stainless tools, remove oil, and keep carbon-steel brushes away from the joint. Contamination is easy to miss. It can later create rust-colored spots.
Moderate heat input is important. Excessive heat may reduce corrosion resistance near the weld by encouraging chromium carbide formation. Short welds, controlled travel speed, and minimal interpass temperature help limit this risk. Low-carbon filler metal, such as 308L-type material, is commonly selected for compatible 304 joints. Shielding gas must fully cover the molten pool and the hot root, especially on thin tubing. A dull gray root often signals poor protection or insufficient purging.
Fit-up deserves attention. A narrow, even gap supports penetration without demanding excessive heat. Tack welds should be clean and spaced evenly, because uneven tacks can pull the joint out of alignment. After welding, remove heat tint mechanically or chemically using a suitable stainless-steel procedure. I sometimes underestimate the effect of a small tack, and that mistake becomes visible only after cooling. Inspect the bead, surrounding discoloration, and backside before service.
How to Weld 304 Stainless Steel Successfully?
Understanding 304 Stainless Steel and Its Welding Characteristics
| Category | Item | Typical Data and Welding Guidance |
|---|---|---|
| Material Overview | Austenitic stainless steel | 304 stainless steel is a chromium-nickel austenitic stainless steel with good corrosion resistance, formability, and weldability. |
| Chemical Composition | Chromium | 18.0–20.0% by mass. Chromium helps form the passive oxide film that provides corrosion resistance. |
| Chemical Composition | Nickel | 8.0–10.5% by mass. Nickel stabilizes the austenitic structure and improves toughness and formability. |
| Chemical Composition | Carbon | Maximum 0.07% by mass for standard 304 material. Lower-carbon 304L is preferred when resistance to weld sensitization is especially important. |
| Chemical Composition | Manganese, silicon, phosphorus, and sulfur | Typical specification limits are manganese up to 2.00%, silicon up to 0.75%, phosphorus up to 0.045%, and sulfur up to 0.030% by mass; iron makes up the balance. |
| Base-Metal Properties | Minimum tensile strength | Approximately 515 MPa for annealed plate meeting common 304 stainless steel specifications. |
| Base-Metal Properties | Minimum yield strength | Approximately 205 MPa at 0.2% offset for annealed plate meeting common 304 stainless steel specifications. |
| Base-Metal Properties | Melting range | Approximately 1,400–1,450°C. Actual melting behavior depends on chemical composition and heat input. |
| Welding Characteristics | General weldability | 304 stainless steel is readily weldable using TIG, MIG/GMAW, SMAW, and resistance-welding processes. Distortion and heat tint must be controlled. |
| Welding Preparation | Cleaning | Remove oil, paint, moisture, oxide, and other contaminants. Use dedicated stainless-steel brushes and tools to prevent carbon-steel contamination. |
| Welding Preparation | Joint fit-up | Maintain consistent joint gap, alignment, and root opening. Excessive gaps increase heat input, shrinkage, and distortion. |
| Thermal Control | Preheating | Normally not required for clean 304 stainless steel. Avoid unnecessary preheating because it can increase distortion and heat exposure. |
| Thermal Control | Interpass temperature | Keep the workpiece cool between passes; a commonly used control limit is approximately 150°C maximum unless the approved welding procedure specifies otherwise. |
| Thermal Control | Heat input | Use the lowest practical heat input that provides complete fusion. Excessive heat increases distortion, oxide formation, and the risk of sensitization. |
| Filler Metal | TIG and MIG filler | ER308L-type filler is commonly selected for welding 304 stainless steel. ER308LSi-type filler may improve bead wetting in suitable MIG applications. |
| Filler Metal | Shielded metal arc electrode | E308L-type electrodes are commonly used for manual arc welding of 304 stainless steel. |
| Shielding Gas | TIG shielding gas | High-purity argon is commonly used. A typical starting flow range is approximately 8–14 L/min, adjusted for nozzle size, joint design, and drafts. |
| Shielding Gas | MIG shielding gas | Argon-rich gas mixtures are commonly used. Small additions of carbon dioxide or oxygen may improve arc behavior, but excessive active gas can increase oxidation and spatter. |
| Process Selection | TIG/GTAW | Provides precise heat control and clean welds, making it suitable for thin sheet, visible joints, root passes, and applications requiring high weld appearance. |
| Process Selection | MIG/GMAW | Offers higher deposition rates than TIG and is suitable for production welding when parameters, shielding, and wire feeding are properly controlled. |
| Process Selection | SMAW | Useful for field and repair work. Keep electrodes dry according to the applicable welding procedure and remove slag completely between passes. |
| Typical Starting Parameters | TIG current for thin sheet | Approximately 35–90 A for about 0.8–2.0 mm material as a starting range. Final settings depend on joint type, polarity, tungsten size, and operator technique. |
| Typical Starting Parameters | TIG current for medium thickness | Approximately 90–160 A for about 2.0–4.0 mm material as a starting range. Use test coupons to confirm penetration and heat control. |
| Welding Technique | Polarity | DCEN is commonly used for TIG welding. MIG welding generally uses DCEP with solid wire; always follow the qualified procedure for the selected process. |
| Welding Technique | Travel speed | Maintain a steady travel speed and avoid excessive weaving. A controlled, narrow bead generally reduces heat input and distortion. |
| Welding Technique | Back purging | Use argon back purging for full-penetration joints where the root surface must remain clean. A gray, black, or heavily oxidized root indicates inadequate protection. |
| Metallurgical Risk | Sensitization | Prolonged exposure to approximately 425–850°C can cause chromium carbide precipitation at grain boundaries and reduce corrosion resistance near the weld. |
| Metallurgical Risk | How to reduce sensitization | Use low-carbon filler, limit heat input and interpass temperature, avoid unnecessary reheating, and use stabilized grades when the service conditions require additional resistance. |
| Post-Weld Treatment | Heat treatment | Post-weld heat treatment is generally not required for ordinary 304 stainless steel fabrication. Any thermal treatment should be specified by the design or welding procedure. |
| Post-Weld Treatment | Cleaning and passivation | Remove slag, spatter, heat tint, and embedded iron after welding. Mechanical cleaning followed by an appropriate passivation treatment can restore surface corrosion resistance. |
| Quality Inspection | Visual inspection | Check for cracks, undercut, overlap, lack of fusion, excessive reinforcement, porosity, arc strikes, and unacceptable heat tint. |
| Quality Inspection | Common non-destructive tests | Liquid penetrant testing is suitable for detecting surface-breaking defects. Radiographic or ultrasonic testing may be selected for internal defects according to thickness and joint design. |
| Safety | Fume control | Use local exhaust ventilation and suitable respiratory protection when required. Stainless-steel welding fumes can contain hazardous metal oxides, including chromium compounds. |
Note: Parameter ranges are typical starting values, not universal production settings. Confirm final values with qualified welding procedures, joint design, material thickness, and applicable codes.